Fully Automated Elastic Rail Clip Production Line
Fully Automated Elastic Rail Clip Production Line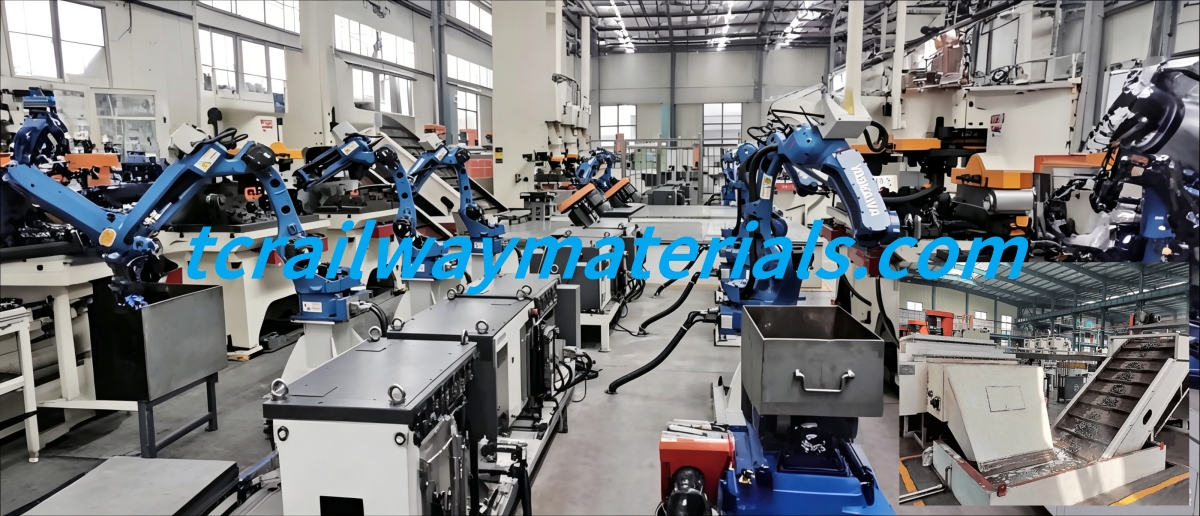
We supply the automated elastic rail clip production line, an intelligent production unit for manufacturing rail spring clips. It adopts robot‑operated material‑handling integrated with a three‑stage hot‑stamping process. The entire production process runs fully automatically, covering raw‑bar feeding, medium‑frequency heating, stamping forming and quenching treatment.It enables you to run reliable non‑stop long‑term production. Furthermore, it boosts your output, while maintaining perfectly consistent finished‑product quality. Moreover, it can deliver 25 railway spring‑clips per minute and produce various spring‑clip models with different interchangeable mold sets. We provide professional skill training for maintenance technicians to help them master mold replacement, equipment troubleshooting and finished product quality inspection. If you have any requirements, please feel free to contact us.
Key Technical Specifications
Applicable Products: Various rail spring clips, including W-type, E-type and Fast-type spring clips
Applicable Raw Materials: 60Si2MnA spring steel and other special spring steels for rail fasteners
Processing Specifications: Raw bar diameter φ13–φ18 mm; customized bar length is available
Application Scenarios: Large-scale spring clip manufacturers and railway fastener component factories
Fully Automated Elastic Rail Clip Production Line Layout Drawing
Production Technology and Automated Layout
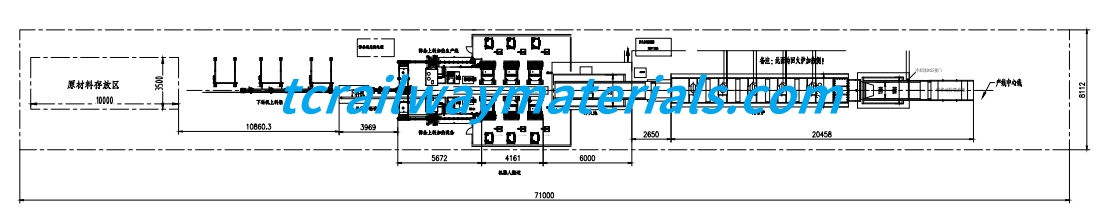
Our railway spring clip production line adopts hot forming technology. Spring steel bars are heated to forging temperature through medium-frequency induction heating, then shaped via three stamping stages to complete thermal forming. Four industrial robots conduct full-process automatic material transfer to realize unmanned continuous production. It runs at a stable production speed of 10–13 pieces per minute, with a single-shift output of 4,000–5,000 pieces, far more efficient than traditional manual production lines.
Full Equipment List of Automatic Elastic Rail Clip Production Line
Section | Item Name | Quantity | Key Features |
Step Automatic Feeding Section | Automatic Loader & Feeding Mechanism | 1 set | Approx 1000 steel bars storage; dual stepper motor servo feeding, buffer pressing structure, multi-fault alarm & communication interface |
Medium Frequency Heating Section | Lifting Loader & Feeding Mechanism | 1 set | Works with loader to feed steel bars into heating coil |
260KW IGBT Medium Frequency Heating Equipment | 1 set | Rated power 260KW, frequency 8–15KHz; Temperature range: 930–1030°C, tolerance ±10°C; multi electrical protection, isolated safety transformer | |
Plate Heat Exchanger | 1 set | Isolate internal & external cooling water, prevent scaling, stabilize heating equipment operation | |
Heating Positioning & Discharging Mechanism | 1 set | Precisely position heated steel bars, ensure stable material pickup by the robot | |
Stamping Forming Section | 80T Punch Press | 3 units | 3-stage step hot stamping, support pre-forming, secondary forming & final forming |
Forming Dies & Auxiliary Positioning Tooling | 5 sets | 5 sets of dies for quick changeover, compatible with W/E/Fast type spring clips | |
Batch of Die Spare Parts | 1 set | Complete set of wear-resistant spare parts, reduce maintenance downtime | |
Infrared Temperature Measuring Device | 2 units | Temp measuring range 400–1400℃; auto reject unqualified workpieces (low/over temp) | |
Yaskawa Handling Robot (Base & Gripper Included) | 4 sets | 4 Yaskawa robots for full-auto workpiece handling, complete full-process transfer from heating to 3 stamping & oil quenching | |
Electrical Control & Safety System | Siemens PLC Control System | 1 set | Connect robots & punch presses via Profibus bus, collect full-process sensor signals |
Main Control Cabinet + Robot Cabinet + HMI Touch Screen | 1 set | Visualize full line operation status, support manual/auto mode switch | |
Safety Interlock System, Safety Light Curtain, Cables & Accessories | 1 set | Man-machine isolation protection, equipment safety interlock, prevent production safety accidents | |
Auxiliary Accessories | Quenching Guide Chute, Scrap Cart | 1 set | Auto feed stamped workpieces into oil quenching process, collect production scraps uniformly |
Automatic Elastic Rail Clip Production Line Layout Diagram
Overview of Functional Zones for Automatic Elastic Rail Clip Production Line
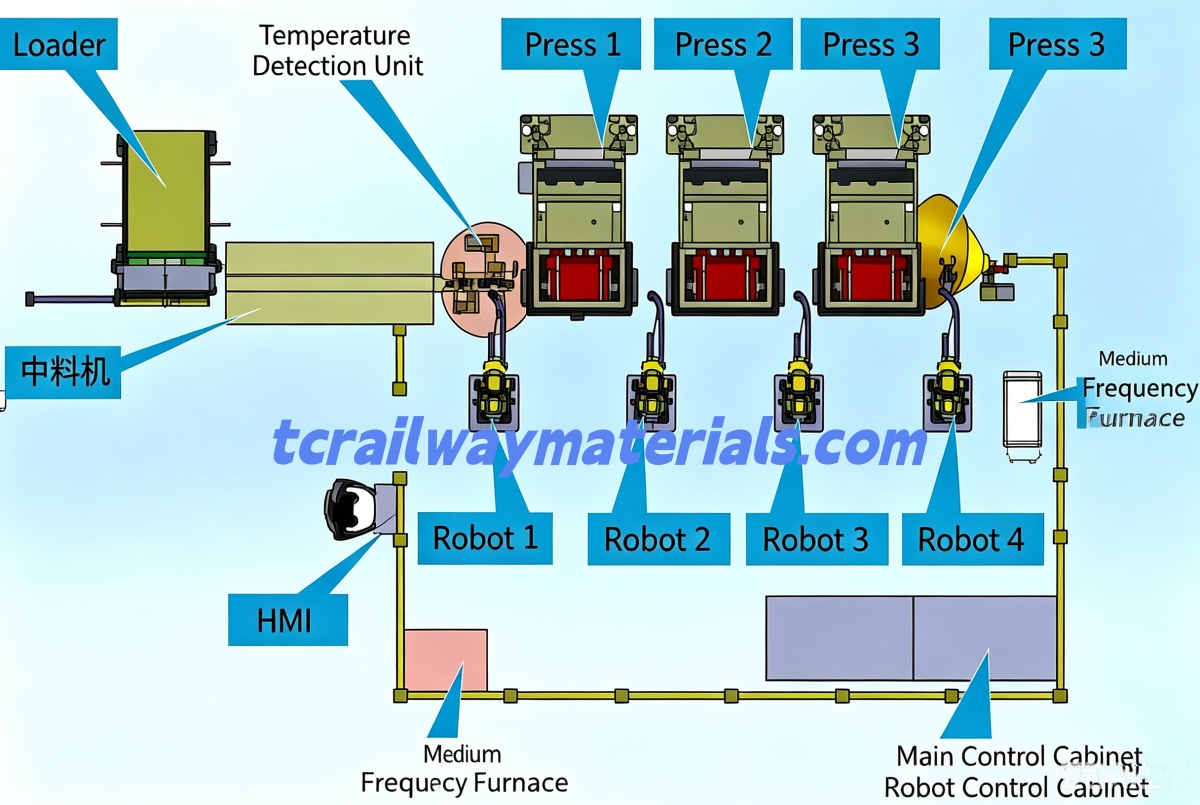
Material Feeding Area: It is located at the far left of the line, and it is fitted with a stepped automatic feeding mechanism for easy raw material refilling.
Heating Zone: It is set right after the feeding section, and it is equipped with a medium-frequency heating furnace and cooling system to sustain continuous heating of steel bars.
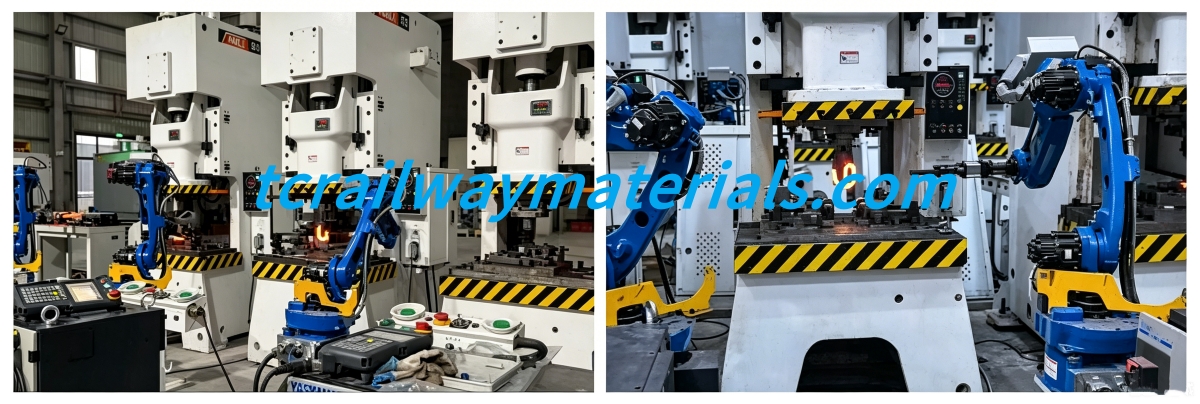
Stamping Forming Area: It is the core production zone of the whole line, and it is fitted with three sequential 80-ton punch presses and 4 handling robots on both sides for fully automatic workpiece transfer.
Quenching & Waste Collection Area: It is situated at the tail end of the line, and it contains quenching guide chutes and scrap carts to transfer stamped parts to the oil quenching process.
Control Area: It is equipped with the main control cabinet, robot cabinets and HMI touch screen, and it allows operators to monitor the full production line operating status in real time.
Elastic Rail Clips Manufacturing Process
1. Raw Material Feeding Process
This line adopts a stepped automatic feeder. It sorts and arranges spring steel bars with diameters from φ13 to φ18, and feeds them into the medium-frequency heating furnace step by step via an adjustable continuous feeding mechanism. The storage bin can hold around 1,000 steel bars to support long-term uninterrupted production.
2. Medium-Frequency Heating Process
Steel bars are heated by IGBT medium-frequency induction heating equipment. The heating temperature is controlled at 930–1030°C with a tolerance of ±10°C. The longitudinal progressive feeding design ensures a minimum output of 20 fixed-length (433 mm) φ13 steel bars per minute. Infrared thermometers detect the temperature of heated bars, and unqualified workpieces will be automatically rejected.
3. First Pre-Stamping Process
Robot 1 transfers heated steel bars from the heating discharge station to the mold of No.1 punch press. It finishes the initial stamping to bend straight steel bars into a rough U-shape. The workpiece temperature must stay above 870°C during stamping.
4. Second Forming Stamping Process
Robot 2 moves the semi-finished workpiece from No.1 press to No.2 press. The second stamping further shapes the U-shaped part into the basic outline of rail spring clip, and forms the preliminary curve of two clip arms.
5. Third Finishing Stamping Process
Robot 3 delivers workpieces from No.2 press to No.3 press. The third stamping performs final shaping to guarantee all dimensions and profiles fully match drawing requirements.
6. Quenching Handling Process
Robot 4 takes finished spring clips out of No.3 press and sends them into the oil quenching guide chute for quenching. This completes the whole hot forming process of rail spring clips. Quenched parts will go through follow-up heat treatment and surface treatment.
Automatic Rail Spring Clip Production Line Technical Parameters
project | parameter | remarks |
production takt | 25 items per minute | Adjust according to product model |
Heating rhythm | ≥20 per minute | Specification: φ13 × 433 |
Workpiece preheating temperature | 930- 1030℃ | |
Stamping Completion Temperature | ≥870℃ |
Basic Production & Raw Material Parameters of Automatic Rail Spring Clip Production Line
Parameter Name | qualification | remarks |
production takt | 25 items per minute | Adjust according to product model |
Applicable bar diameter: | φ13-φ18mm | |
Applicable bar length | customizable | Standard: 433 mm |
Main Components of Automatic Rail Clip Manufacturing Line
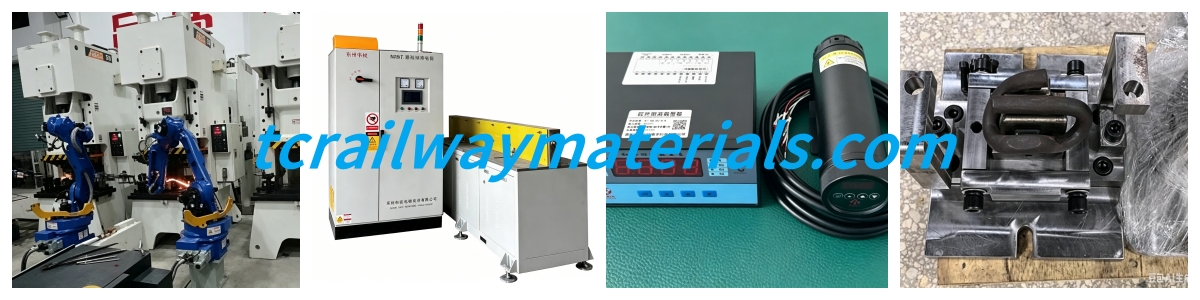
1. Full Automatic Stamping & Robot Operation Scene,
2. 260KW IGBT Medium Frequency Heating Unit,
3. Online Infrared Temperature Measuring System (Sensor + Digital Display Meter),
4. Interchangeable Forming Dies (Pre-forming & Sizing Dies),
5. Siemens PLC Bus Control Schematic Diagram
Detailed Technical Highlights of Core Components for Automatic Rail Clip Manufacturing Line
1. 260KW IGBT Medium Frequency Heating Unit:
Rated power 260KW, frequency range 8–15KHz, power adjustable 10%–100% continuously
Complete multi-protection: overcurrent, overvoltage, phase loss, water temperature & water pressure protection
Automatic frequency tracking, adapts to ±30% ~ +10% grid voltage fluctuation
Built-in isolation transformer to avoid electric hazard from coil insulation damage
High efficiency ≥95%, low magnetic radiation (≤12μT within 5m radius)
Dual water cooling system for long service life, stable continuous operation 24h
2. Online Infrared Temperature Measuring System:
Measuring range 400–1400℃, precision ±1% reading, response time <100ms
3-way automatic sorting alarm (high temp / qualified / low temp), auto reject unheated bars
IP65 protection, RS485 & 4–20mA signal output, can connect with PLC system
3. 4 Units Yaskawa Robots Equipped with Full Safety Interlock System
4 Yaskawa robots with custom grippers, independent transfer for each stamping station
Siemens Profibus bus communication between robots and 80T punch presses
Safety light curtain + full interlock system to prevent man-machine collision
Frequently Asked Questions About Our Rail Clip Automated Production Line
Q1: Can we customize the production line for different sizes of rail clips?
A: Yes. Our fully automatic rail clip forming line supports full customization. We adjust forming dies, heating power and robot stroke according to your required specifications, covering E-type, W-type and SKL elastic rail clips. Matching interchangeable molds will be delivered together with the machine.
Q2: How long does mold replacement take?
A: Standard mold change only takes 15–25 minutes. All dies adopt quick locking structure with unified base, no secondary calibration needed after replacement, greatly cutting production downtime.
Q3: What is the power consumption of the whole line?
A: Equipped with energy-saving 260KW IGBT medium frequency heating unit, Yaskawa robots and PLC energy-saving control. Continuous running average power consumption is about 210–240 kWh/h, with automatic standby power-off to reduce idle loss.
Q4: How many workers are required to operate the production line?
A: Only 1 skilled operator is enough. The automatic system completes feeding, heating, stamping and unloading automatically. The worker only needs to replenish steel bars and do routine inspections.
Q5: What is your equipment warranty policy?
A:
Whole machine: 1-year warranty from commissioning;
Core parts (Yaskawa robots, Siemens PLC, heating unit, infrared thermometer): 12-month warranty;
Mold wearing parts are not covered by free warranty, we provide cost-price replacement and lifetime technical support;
Free year-round remote troubleshooting, overseas on-site maintenance available on request.
 English
 Русский